Export-Grade String Instruments & Protective Hardware
Our integrated manufacturing plants produce CE-compliant fretted and traditional folk instruments engineered to stringent acoustic specifications, moisture-controlled stability tolerances, and REACH-certified finish formulations.
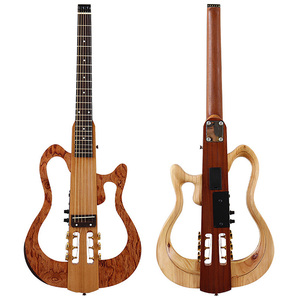
39 Inch Foldable Travel Plug Guitar 6-String Headless & Detachable Design
Patented modular aerospace hinge, onboard preamp headphone monitor, active noise-isolated pickup circuit.
Product Specs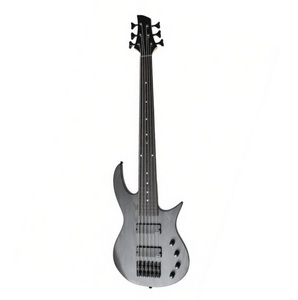
Weifang Rebon 6 String Fretless Electric Bass Guitar With Ashwood Body
Solid swamp ash resonant body, continuous ebony fingerboard radius, dual humbucker active EQ system.
Product Specs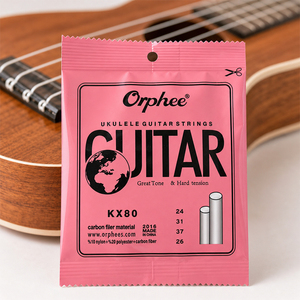
Wholesale Orphee KX80 Carbon Ukulele Guitar Strings China Matte Finish
High-density extruded fluorocarbon, matte non-slip surface, precise pitch calibration, high tensile elasticity.
Product Specs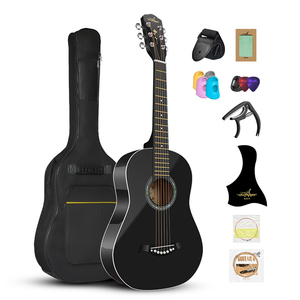
Wholesale Custom Glossy Travel 30 34 36 Inch Folk Acoustic Guitar
Ergonomic scaled neck, non-toxic EN 71-3 gloss finish, low-action setup tailored for student ergonomics.
Product Specs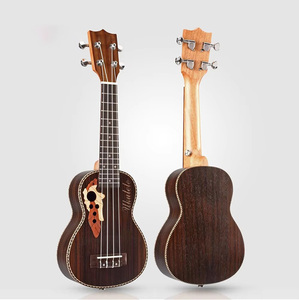
China Factory OEM Rosewood Ukulele Set - Tenor/Baritone/Soprano
Selected tonal tonewood soundboard, bone nut & saddle, closed gear machine heads, laser-cut bracing.
Product Specs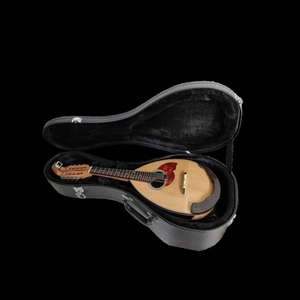
Premium Bowl-Back Mandolin High-Pitched 8-String Bowl Shape Mandolin
Traditional multi-rib maple vaulted back, solid spruce top, hand-carved bridge, warm European classical timbre.
Product Specs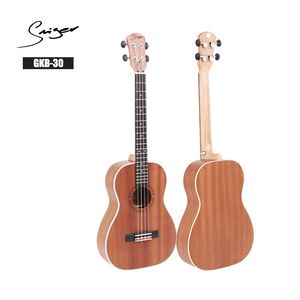
Wholesale Musical Instruments 30inch Sapele Baritone Ukulele
Deep resonant chamber, quarter-sawn African sapele body, D-G-B-E linear tuning stability, satin open-pore finish.
Product Specs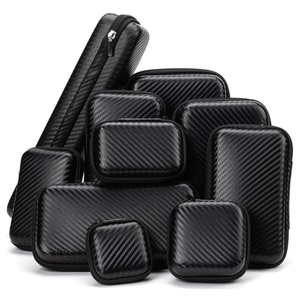
Wholesale Custom Shell Carbon Fiber Tool Storage Bag EVA Case Hard Shell
Waterproof ballistic EVA composite, custom high-density velvet lining, shock absorption rating IP65 compliant.
Product SpecsAcoustic Physics & Mechanical Architecture of Open Back Banjos
In traditional bluegrass and old-time clawhammer music, the open back banjo (often referred to as an old-time or frailing banjo) occupies a distinctive acoustic niche characterized by warm lower-midrange frequencies, rapid transient decay, and wide dynamic responsiveness. Unlike resonator-backed models that feature an enclosed chamber and metal sound flange engineered to compress and project high-frequency sound forward in loud ensemble settings, the open back banjo relies on direct mechanical wave propagation from an unsealed 11-inch or 12-inch rim assembly.
For institutional musical instrument importers, large-scale educational tender contractors, and global brand distributors, evaluating a manufacturing facility requires looking beyond aesthetic appearance to examine the underlying acoustic physics. The energy pathway begins when a string is plucked: vibrational energy transfers across the compensated maple/ebony bridge to the pre-tensioned synthetic or calfskin head, radiating through the tone ring directly into the wood rim, which acts as the acoustic frame. Without a reflective resonator back, soundwaves disperse omnidirectionally, interacting directly with the player's torso. This damping effect suppresses harsh upper-harmonic spikes between 3.5 kHz and 5.5 kHz, yielding the authentic "woody, plunky" timbre coveted by clawhammer purists.
Our OEM/ODM manufacturing facility maintains specialized tooling calibrated to control every acoustic variable in open-back lutherie. Standard mass-production facilities frequently suffer from rim deformation (out-of-round warping) after transoceanic shipping due to unequal tension across bracket shoes. We eliminate this failure mode through computer-controlled hydraulic rim-forming presses, seasoning all laminated maple and walnut hoops in climate-stabilized chambers for 45 days prior to final CNC turning. This process ensures out-of-round tolerances remain within a stringent ±0.15mm margin across seasonal humidity shifts ranging from 20% to 85% RH.
Rim Architecture
Constructed with Grade-A Hard Rock Maple or Black Walnut. Multi-ply laminate design hot-pressed under 12 MPa hydraulic load guarantees zero delamination and optimal acoustic resonance transfer.
Tone Ring Dynamics
Options range from rolled brass round-rod tone rings to precision Whyte Laydie and Tubaphone alloy castings, engineered to calibrate upper harmonic sparkle without inducing high-register harshness.
Dual Coordinator Rods
Heavy-duty, lead-free brass or stainless-steel dual coordinator rod system permits micro-action adjustments while locking the rim in structural equilibrium under high-tension steel stringing.
Frailing Scoop Necks
Custom CNC-machined neck extension scoops past the 17th or 19th fret allow comfortable right-hand over-the-neck frailing techniques without thumb-pick strike collisions against fretwire.
European Market Compliance: CE Marking, RoHS, REACH & CITES
A primary point of failure for Western musical instrument brands sourcing from unvetted suppliers is regulatory non-compliance at European customs borders. In the European Union, entering musical instruments and accessories into the single market requires compliance with multiple harmonized directives. While an acoustic instrument does not fall under the Low Voltage Directive (LVD) or Electromagnetic Compatibility (EMC) Directive unless fitted with active electronic preamplifiers, all integrated packages, electro-acoustic variations, gig bags, cases, and finished hardware coatings are strictly subject to CE, REACH, and RoHS protocols.
Our OEM manufacturing lines operate under comprehensive ISO 9001:2015 quality frameworks, maintaining third-party laboratory verification (SGS, TÜV SÜD) to safeguard our supply chain partners against customs impoundment, fines, or brand-damaging recalls.
| Compliance Standard | Target Component / Material | Regulatory Mandate & Limit | Factory Verification Protocol | Audit Status |
|---|---|---|---|---|
| RoHS Directive 2011/65/EU & (EU) 2015/863 | Electro-galvanized bracket shoes, tuning gears, truss rods, solder joints | Lead (Pb) < 0.1%, Cadmium (Cd) < 0.01%, Hexavalent Chromium (Cr VI) < 0.1% | XRF spectrometry batch screening + ICP-OES wet chemistry verification | 100% Certified |
| REACH Regulation (EC) 1907/2006 | Polyester/PU finishes, synthetic Mylar banjo heads, EVA protective shells | SVHC candidate list screening < 0.1% w/w; Phthalate ban (DEHP, DBP, BBP, DIBP) | Gas Chromatography-Mass Spectrometry (GC-MS) for plasticizers & volatile organics | SVHC Compliant |
| EN 71-3 Safety of Toys Standard | Surface lacquers, neck finishes, edge binding, stained wood tonewoods | Migration limits for 19 toxic heavy metals (aluminum, antimony, arsenic, barium, etc.) | Simulated gastric acid migration analysis performed on dry lacquer scrapings | Full Pass |
| CITES Appendices I & II / EUDR 2023/1115 | Fingerboards, bridges, decorative veneers, peghead overlays | Traceability of Dalbergia species; complete chain-of-custody timber verification | Legal harvest documentation, pre-issued phytosanitary permits, FSC-certified supply chains | Legally Vetted |
When shipping banjos complete with gig bags or carbon fiber EVA cases (such as our SKU: ACC-EVA-CF), European border enforcement officers routinely test for polycyclic aromatic hydrocarbons (PAHs) in rubber handles and foam padding. By partnering with a factory that proactively formulates with odorless, medical-grade EVA and REACH-certified adhesives, importers protect both end-user health and corporate legal liability.
Future Procurement & Engineering Trends in Folk Instruments
The global folk stringed instrument market is undergoing a structural transformation driven by changing player demographics, evolving environmental legislation, and automation in precision lutherie.
Sustainable Alternative Tonewoods & Torrefaction
Due to escalating CITES scrutiny and the European Union Deforestation Regulation (EUDR), commercial brands are migrating from traditional East Indian Rosewood (Dalbergia latifolia) fingerboards toward engineered techwoods, thermally modified (torrefied) hard maple, and African blackwood substitutes. Torrefaction—baking timber in an oxygen-deprived kiln at 180°C to 220°C—crystallizes hemicellulose, permanently reducing hygroscopic shrinkage while replicating the rich acoustic projection of century-old vintage lutherie woods.
Hybrid Electro-Acoustic Modular Transducers
Traditional open back banjos are notoriously difficult to amplify in modern live performance without generating severe acoustic microphonics and low-frequency feedback loops. The next procurement cycle is heavily favoring models pre-routed for concealed internal condenser capsules or bridge-embedded piezo transducers. These systems incorporate passive impedance-matching circuits, enabling musicians to plug directly into acoustic stage amplifiers or USB digital audio workstations without altering the instrument's classic silhouette.
CNC Precision Neck Geometry & Plek Fret Dressing
Manual fret leveling introduces human variance across production batches. Leading suppliers are investing in multi-axis robotic CNC carving cells and computerized fretting stations. By crowning fret wire under simulated string tension with sub-micron accuracy, manufacturers eliminate dead notes, string buzz, and fret sprout. This high level of build consistency reduces downstream warranty claim rates for Western music distributors to below 0.35% of total import volume.
Rooted in Over 150 Years of American Stringed Craft
Oscar Schmidt’s storied history dates back to Jersey City, New Jersey, in 1871. We combine time-tested American folk lutherie heritage with state-of-the-art lean manufacturing, delivering scalable OEM/ODM solutions to global distributors.
Full Category Coverage
Consolidate your procurement across our complete fretted instrument catalog. Source open back and resonator banjos, autoharps, bowl-back mandolins, soprano-to-baritone ukuleles, acoustic guitars, travel instruments, and custom EVA hard bags on a single combined container bill of lading.
Rigorous Factory QA Audits
Every open back banjo undergoes three distinct quality checkpoints: incoming timber moisture verification (stabilized to 6%–8% equilibrium moisture content), laser interferometry fret plane analysis, and an acoustic sound-check before entering custom humidity-sealed inner packaging.
OEM/ODM Customization Flexibility
Tailor your banjo specifications to your target demographic. We provide custom scale lengths (from 19-fret tenor to 22-fret standard 5-string), custom peghead inlays with mother-of-pearl or abalone, planetary vs. vintage geared tuners, and custom frailing scoop dimensions.
Frequently Asked Questions for B2B Importers
Clear, direct answers regarding minimum order quantities, testing verification, customs documentation, and logistics management.
What specific test certificates are delivered with CE-certified open back banjo shipments?
What are the minimum order quantities (MOQ) for custom private-label banjos?
How does your factory prevent wood rim warping and fret sprout during sea freight?
Can your factory supply instruments in true left-handed configurations?
What are typical production lead times for standard vs. OEM custom production?
Partner with an Established Stringed Instrument Manufacturer
Looking to expand your private label line with CE-compliant, premium open back banjos, autoharps, mandolins, or folk string accessories? Connect with our senior engineering and export sales team to request comprehensive OEM price catalogs, physical material samples, and factory compliance dossiers.
Contact Us