Top Industrial Banjo Protection Systems
Engineered specifically for 4-string tenor, 5-string bluegrass, and 6-string hybrid banjos. Our cases feature custom-formed neck cradles, bridge relief chambers, and heavy-duty hardware built for global distributor distribution.
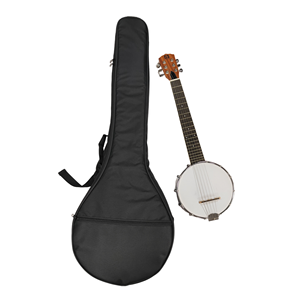
40 Inch 1cm Thick Music Instrument Nylon Gig Bag Customized Logo Big Easy Travel Banjo Bag
- Outer Fabric: 600D Ballistic Nylon
- Padding: 10mm High-Density EPE
- Compatibility: Open-Back / Resonator
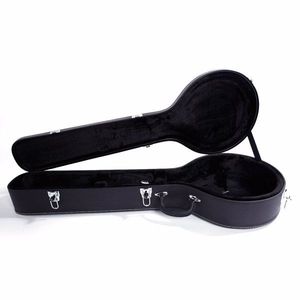
Replace D0100XUV9V7 Black Microgroove Pattern Leather Wood Banjos Case 5-String 6-String
- Core Structure: 5-Ply Cross-Grain Plywood
- Skin Finish: Microgroove PVC Leather
- Interior Lining: Plush Velveteen Foam
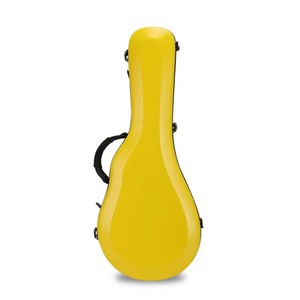
High Quality Real Mission Yellow Fiberglass Banjo Case Zipper Closure Customized Logo Instrument Box Featuring Thickened Inner
- Outer Shell: High-Strength Fiberglass
- Suspension: Molded High-Resilience EVA
- Seal Type: Heavy Weatherproof Zipper
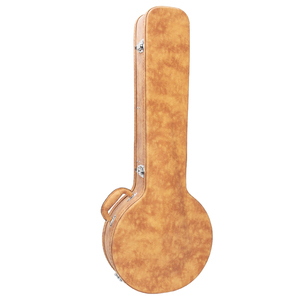
Factory Direct Deluxe Wood Hard Case for Banjo Covered With PVC Leather High Quality Instruments Case
- Lid Profile: Engineered Impact Archtop
- Hardware: Gold-Plated Draw Latches
- Compartment: Capo, Pick & Tuner Bay
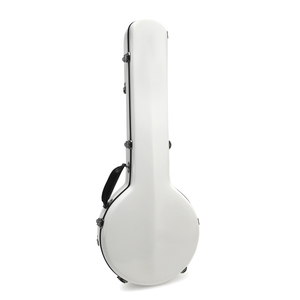
SUN-OBJ WH Rm Rainbow Musical Instruments Wholesale High End Musical Instruments Accessories Fiber Glass Banjo Case
- Shell Matrix: Compression-Molded FRP
- Protection: Anti-Crush 150kg Rating
- Latches: Chrome Heavy-Duty Latches
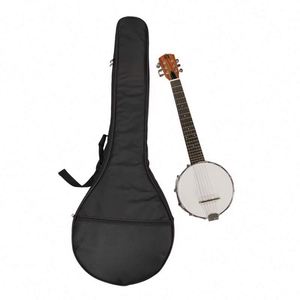
Free Sample 40 4inch 1cm Thick Music Instrument bag Gig Bag Customized Logo Big Easy Travel Banjo Bag
- Carry System: Ergonomic Backpack Straps
- Reinforcement: Rubberized Base Armor
- Weight: 1.15 kg (Super Ultralight)
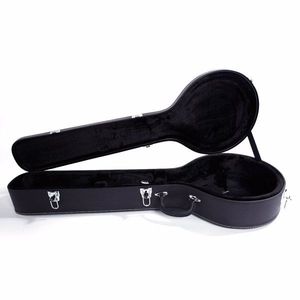
Replace 48950444 Black Microgroove Pattern Leather Wood Banjos Case 5 & 6 String Musical Instrument Bags and Protection
- Fitment: 11" & 12" Resonator Rims
- Rim Cradle: 360° Shock Ring Isolation
- Lock: Integrated Key Locking Latch
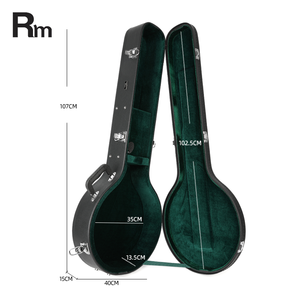
Raibonw High Quality Banjo Instrument Case OEM ODM Plywood and Leather Material Banjo Bags & Cases
- Exterior: Vintage Tweed or Custom Tolex
- Foam Density: 35 kg/m³ High Recovery PU
- Customization: Embossed Leatherette Badge
Structural Integrity Analysis: Overcoming Banjo Load Dynamics
Unlike acoustic guitars where mass is evenly distributed along the soundboard, the banjo presents a profound mechanical challenge for case manufacturers. A professional 5-string banjo concentrates 75% of its total weight (often exceeding 5.5 to 6.5 kg) directly inside the circular rim, driven by heavy cast bronze tone rings and steel coordinator rods.
Radial Perimeter Ring Defense
Standard acoustic case shells distort under localized perimeter stress. Our banjo hardshells utilize proprietary 5-ply to 7-ply cross-banded Birch and Russian Poplar veneers, curved under continuous high-frequency hydraulic pressure. This prevents ring-warping and protects the delicate tension hooks and brackets from impact misalignment.
- Cross-laminated multi-directional shear strength
- Zero-tolerance circular cavity stability
- Lateral drop shear absorption rating > 1200 N
Suspended Floating Bridge Relief
The banjo bridge rests solely under string downbearing on a flexible Mylar or calfskin head. If case padding puts direct downward pressure on the bridge, the head stretches or ruptures. Our cases engineer an arched lid cavity with specialized cantilever contouring, ensuring 18mm to 25mm of non-contact clearance above the bridge tip.
- Zero downward load on bridge compensation zone
- Dual neck-cradle elevation blocks (Nut & Heel)
- Head tension preservation under long cargo transits
5th-String Peg Channel Relief
Traditional 5-string banjos feature a geared tuner protruding perpendicularly from the neck at the fifth fret. Standard generic cases routinely snap this peg during transit. Our molds feature a dedicated CNC-milled 5th-peg relief channel, eliminating lateral contact while stabilizing the fingerboard.
- Asymmetric left-side recess geometry
- High-density micro-velveteen cushioning
- Compatible with standard and planetary geared pegs
| Material Engineering Variant | Shell Density (kg/m²) | Crush Resistance (kg) | Thermal Latency (ΔT / hr) | Ideal B2B Market Segment |
|---|---|---|---|---|
| 5-Ply Arched Poplar/Birch (Tolex) | 4.80 - 5.20 | 110 - 130 kg | 0.65 °C/hr (Superior) | Heritage OEM Brands, Traditional Retail Showcases |
| Vacuum-Infused Fiberglass (FRP) | 3.20 - 3.60 | 160 - 200 kg | 0.48 °C/hr (Moderate) | Touring Professionals, Air Freight Flight Cases |
| High-Impact Molded ABS Shell | 2.90 - 3.30 | 90 - 110 kg | 0.40 °C/hr (Standard) | Educational Institutions, High-Volume E-Commerce |
| 600D / 1680D Ballistic Cordura Bag | 1.10 - 1.45 | Drop cushioned (EVA) | 0.22 °C/hr (Low) | Urban Commuters, Entry-to-Intermediate Bundles |
Strategic Banjo Case Procurement Trends (2025–2030)
International musical instrument supply chains are undergoing structural shifts driven by freight density economics, tightening environmental regulations (RoHS/REACH), and evolving end-user mobility demands.
Volumetric Freight Optimization & Nesting Architecture
Rising sea freight rates and 40ft HQ container constraints require suppliers to optimize dimensional weight. Leading Chinese manufacturers are developing nested shell geometries and quick-release modular handle brackets, increasing container loading capacity from 480 units to over 640 units per 40ft HQ—a direct 25% reduction in landed shipping costs per unit for international distributors.
Eco-Compliant Bio-Resins & Recycled Polymers
With the European Union's corporate sustainability reporting directive (CSRD) taking full effect, instrument cases built with toxic formaldehyde glues or high-VOC adhesives are facing customs rejection. Future procurement mandates water-based polyurethane adhesives, recycled RPET interior velveteen, and bio-based composite exterior resins without compromising flexural rigidity.
Smart Hygrometric Microclimate Integration
Banjo wood rims and multi-piece maple necks are hyper-sensitive to relative humidity swings (RH 45%-55% optimal). Sourcing departments are moving away from passive analog dials toward integrated Bluetooth IoT hygrometer modules embedded in the storage neck box, sending real-time environmental alerts to players' smartphones and preventing moisture-induced neck twist.
The Premier Banjo Protection Partner for Global Brands
Founded on rigorous acoustic engineering standards and serving premier fretted-instrument brands worldwide, our manufacturing facilities merge artisanal woodworking precision with automated aerospace composite tooling. Banjo instruments require distinct anatomical care—ranging from 11-inch flathead rings and 12-inch open-backs to extended archtop resonator flanges.
We do not adapt generic guitar cases; we construct dedicated banjo tooling that ensures precision-calibrated balance points, preventing neck dive when carried and guaranteeing seamless drop protection.
In-House Tooling & Mold Workshop
Rapid 3D CAD modeling, CNC pattern cutting, and mold fabrication within 14 business days.
Stringent ASTM Drop Testing
Every case design passes ISTA-1A drop tests and 150kg uniform crushing pressure before serial signoff.
Scalable Volume Delivery
Monthly production of 20,000+ hardshell cases and 40,000+ gig bags across modernized automated production lines.
Full OEM/ODM Branding Support
Custom silk-screen, heat-debossed leatherette badges, CNC engraved latches, and signature interior velvet colors.
Quality Assurance & Compliance Protocol
Our production lines follow ISO 9001:2015 quality protocols. Every production run undergoes moisture content checks (wood moisture stabilized strictly between 8% and 11% to prevent fungal blooms or structural cracking during trans-oceanic shipping), hardware salt-spray salt corrosion tests (minimum 72 hours), and zero-VOC degassing procedures before final packaging.
Certified Export Standards:
- REACH SVHC Compliant
- RoHS 2.0 Hardware
- FSC Certified Wood Options
- ISTA 1A Transit Tested
- Formaldehyde Free E0 Adhesives
Frequently Asked Questions for B2B Buyers
Key inquiries regarding minimum order quantities, customization protocols, shipping optimization, and quality assurances for banjo cases and gig bags.
What are your standard Minimum Order Quantities (MOQ) for custom OEM banjo cases?
How do you guarantee proper fitment between Open-Back and Resonator banjo profiles?
What transit drop tests and stress standards do your instrument cases adhere to?
How do you resolve moisture and mold issues during 30-45 day ocean freight transits?
What customization options are available for OEM branding and private labeling?
What is the standard production lead time from sample confirmation to full container shipment?
Accelerate Your Musical Instrument Case Supply Chain
Whether you need custom-branded hardshell flight cases for your signature banjo line or high-velocity travel gig bags for mass-market retail, our engineering team is ready to provide 2D/3D CAD mockups, material swatch books, and competitive CIF/FOB wholesale pricing.