Featured Musical Instruments & Professional Luthiery Hardware
Examine our verified high-durability instrument cases, OEM electric & acoustic-electric builds, precision accessories, and tonally balanced string formulations manufactured under strict QA protocols.
Global Industry Analysis: Acoustic-Electric Guitar Sourcing Dynamics
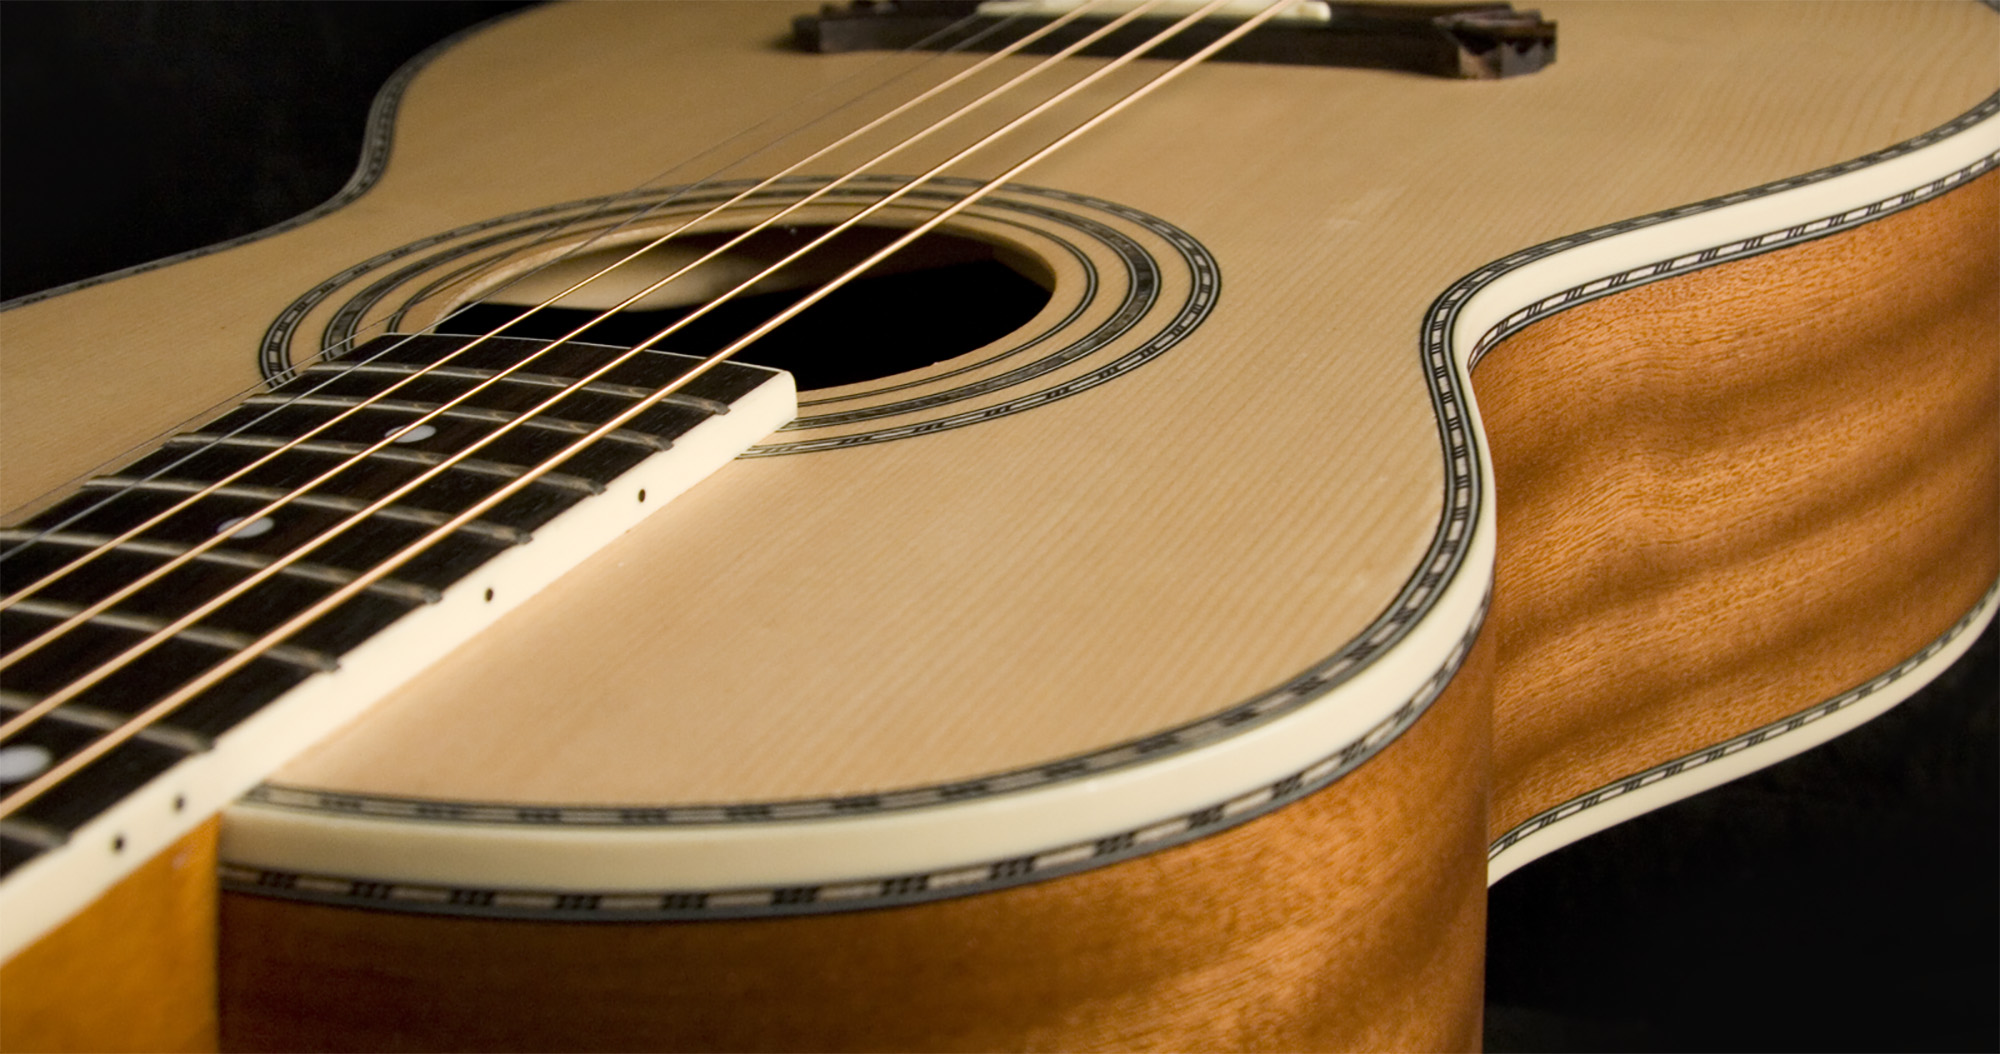
In the competitive landscape of musical instrument retail, institutional supply chains, and private-label e-commerce brands, identifying an elite acoustic electric guitars factory & supplier demands far more than surface-level aesthetic appraisals. The modern acoustic-electric guitar exists as a complex electro-acoustic hybrid: an organic resonance chamber governed by centuries-old lutherie principles, married seamlessly to micro-voltage transduction electronics, discrete Class-A preamplifiers, and modern feedback-rejection micro-circuitry.
For enterprise procurement officers, brand managers, and chain distribution networks, product defects or environmental destabilization can permanently damage brand equity. An acoustic-electric instrument undergoes intense dynamic stress—string tension exceeding 75 to 90 kilograms across the bridge—while simultaneously requiring stable humidity equilibrium inside the tonewood cell structures. When amplified via under-saddle piezoelectric transducers (UST), microphonic anomalies, fret buzz, uneven string balance, and impedance mismatches are magnified tenfold through acoustic amplifiers and direct-injection (DI) audio consoles.
This comprehensive industry white paper establishes clear technical frameworks for auditing acoustic-electric guitar manufacturing facilities. We examine international production hubs, compare the top manufacturing leaders, dissect acoustic engineering tolerances, explore next-generation smart pickup architectures, and provide direct procurement answers regarding CITES compliance, MOQ economics, and kilned-tonewood moisture stabilization.
Tonewood Stability & Kiln Drying
Moisture content regulation between 8% and 10% through computer-monitored dehumidification chambers to prevent top sinking, neck warpage, and bridge lift during cross-continental maritime transit.
Acoustic Voicing & Scalloped Bracing
Precision parabolic and forward-shifted X-bracing geometries engineered via multi-axis CNC routers, voiced to maximize acoustic headroom while suppressing feedback across standard 80Hz–250Hz live stage resonance modes.
Transducer & Preamp Calibration
Integration of high-impedance copolymer piezoelectric bridge elements matched with ultra-low-noise active preamps, chromatic tuners, phase inverters, and calibrated saddle slot routing down to 0.01 mm depth flatness.
Top 10 Acoustic Electric Guitars Factory & Supplier Profiles
An audited breakdown of tier-1 global manufacturing enterprises, evaluated on annual output capacity, automated CNC capability, tonewood aging standards, and international OEM/ODM certifications.
| Rank | Manufacturer / Supplier | Manufacturing Base | Core Strengths & Specialization | Production Capacity | Key Certifications |
|---|---|---|---|---|---|
| 01 | Oscar Schmidt / JAM USA Lutherie Div. | Global Hubs & Asian OEM Lines | Since 1871 heritage; Autoharp®, high-precision acoustic-electric Dreadnought, Concert & Folk instruments; US QC control. | 350,000+ units/yr | ISO9001, CITES, RoHS, CE |
| 02 | Cort Guitars (Cor-Tek Musical) | Indonesia & China | Massive automated electrostatic finishing lines; high-volume OEM manufacturing for multiple global top-ten acoustic labels. | 1,000,000+ units/yr | ISO9001, ISO14001 |
| 03 | Samick Musical Instruments | Indonesia | Vast wood drying and processing infrastructure; acoustic-electric hollow-body and archtop construction specialization. | 600,000+ units/yr | FSC Chain of Custody, ISO9001 |
| 04 | Dyna Gakki Production Corp. | Japan | High-end luthiery, tight-grain Japanese cedar and spruce soundboards, boutique acoustic-electric craftsmanship and PLEK fret dress. | 80,000+ units/yr | Master Luthier Guild Standards |
| 05 | Grand Reward Education & Music | Guangdong, China | High-precision acoustic-electric OEM facility for premium Western brands; advanced UV curing and laser inlay cutting. | 400,000+ units/yr | ISO9001, CITES Certified |
| 06 | Godin Guitars Manufacturing Hub | Quebec, Canada | Sustainable North American tonewoods (Wild Cherry, Silver Leaf Maple); multi-voice synth-access acoustic-electric pioneers. | 150,000+ units/yr | Lacey Act Compliant, FSC |
| 07 | Furch Guitars Modern Workshop | Velké Němčice, Czech Republic | Proprietary soundboard voicing algorithms, individual top tuning, carbon-reinforced neck systems (CNR System). | 25,000+ units/yr | EU Green Certification, CITES |
| 08 | Farida Guitars (Global Luthier Mfg) | Huizhou, China | Computerized climatic cleanrooms; specializes in vintage-spec acoustic-electric dreadnoughts and modern bevel cutaways. | 180,000+ units/yr | ISO9001, BSCI Audited |
| 09 | Wildwood Musical Instrument Works | Shandong, China | High-efficiency OEM electric and acoustic-electric entry kits, composite fretboards, flexible rapid prototype tooling. | 300,000+ units/yr | CE, RoHS, REACH |
| 10 | Pao Sheng Musical Instruments | Taiwan & Dongguan | High-end acoustic-electric composite carbon fiber guitars, weather-proof travel acoustics, miniature internal preamps. | 120,000+ units/yr | ISO9001, REACH |
Future Sourcing & Technological Trends in Acoustic-Electric Production
How regulatory pressures, tonewood scarcity, digital signal processing, and automated precision machining are redefining the supply chain landscape.
Procurement professionals must adapt to four pivotal macro shifts currently transforming acoustic-electric guitar manufacturing worldwide. Driven by environmental treaties, evolving consumer sonic tastes, and digital connectivity, smart suppliers are redesigning their factory floors to deliver lighter, more resonant, yet road-ready electrified acoustic models.
1. Torrefaction & Engineered Wood Alternates
With stringent CITES Annex II regulations on Rosewood (Dalbergia) and genuine Mahogany, leading factories utilize thermo-cured "baked" tonewoods (torrefied Sitka spruce, thermally modified birch) and high-density technical woods (Richlite, composite ebony). Torrefaction crystallizes internal wood resins, simulating 50 years of natural cellular aging, boosting projection while providing near-zero hygroscopic sensitivity.
2. Dual-Source Transduction & Internal DSP
Single under-saddle piezo ribbons are being supplanted by dual-source sensing arrays: combining under-saddle transducers with internal cardioid boundary condenser microphones or acoustic soundboard body-sensors. Factories now integrate micro-DSP preamps capable of onboard IR (Impulse Response) cabinet emulation, Bluetooth wireless pairing for real-time mobile app equalization, and USB-C direct-recording digital audio outputs.
3. High-Precision PLEK & Robotic UV Curing
Modern tier-1 facilities feature computerized PLEK fret-dressing stations that simulate real string tension to level frets down to 0.005 mm accuracy. Furthermore, automated electrostatic robotic arms apply ultra-thin UV-cured polyurethane or polyester finishes (under 0.15 mm thickness), allowing unrestricted soundboard vibration while curing instantly without volatile solvent emissions.
150+ Years of American Stringed Instrument Engineering Since 1871
Originating in Jersey City, New Jersey, in 1871, the Oscar Schmidt company defined accessible American string craft, engineering the iconic Autoharp® and bringing concert-grade folk instruments into classrooms, recording studios, and stages globally. As part of JAM USA LLC and operating alongside sister brand Washburn, our manufacturing ecosystem pairs historic artisan lutherie with modern high-capacity scalable OEM infrastructure.
-
Comprehensive Fretted Instrument Range: Full-catalog manufacturing spanning acoustic guitars, acoustic-electric dreadnoughts, Autoharps®, banjos, mandolins, ukuleles, electric basses, and fitted fiberglass cases.
-
Integrated Left-Handed Production Lines: Dedicated left-handed tooling setups ensuring true left-handed bracing patterns, bridge angling, and nut intonation without compromise.
-
Complete International Regulatory Compliance: Strict Lacey Act, CITES Appendix II verification, REACH chemical certification, and ISO 9001 quality management across all contract facilities.
-
Global Authorized Service Network: Robust post-sale support, standardized replacement components, authorized service centers, and factory warranty backing for global retail and distribution partners.
Acoustic Electric Guitars Factory & Sourcing FAQ
Authoritative answers to the key technical, financial, and logistical questions encountered when contracting OEM/ODM acoustic-electric manufacturing.
What is the standard Minimum Order Quantity (MOQ) for custom OEM acoustic-electrics?
Standard OEM production minimums generally start at 100 to 300 units per model specification (tonewood combination, finish, body shape). For catalog-standard private labeling or existing tooling configurations, MOQs can be negotiated at 50 units. Boutique high-tier solid-wood builds with specialized onboard electronics or custom laser rosette inlays often accommodate lower initial pilot runs to facilitate pilot retail distribution.
How do certified factories prevent bridge lifting and under-saddle pickup imbalance?
Bridge lifting is eliminated through ultrasonic glue-joint moisture inspection and gluing the bridge directly onto bare wood prior to top lacquering. To prevent uneven string output in under-saddle piezo pickups, the bridge saddle slot must be CNC-routed to an absolute bottom flatness tolerance of ±0.01 mm. Any saddle concavity causes uneven pressure on individual piezo crystals, resulting in quiet or boomy strings.
What quality certifications and timber documentation are required for North American & European import?
Importers must verify full compliance with the US Lacey Act and EU Timber Regulation (EUTR/EUDR), requiring documented chain of custody from forestry concession to sawmill. If species such as Dalbergia latifolia (Indian Rosewood) or Bubinga are utilized, formal CITES re-export certificates are mandatory. Electronic preamps, onboard tuners, and pickup assemblies must carry CE, FCC, and RoHS certifications ensuring lead-free soldering and electromagnetic shielding.
How does climate conditioning protect shipments during sea freight?
Tier-1 factories enforce a 72-hour equilibrium period inside relative humidity (RH) controlled packing chambers stabilized at 45%–50% RH and 22°C. Instruments are packaged with military-spec silica desiccant gel packs inside sealed heavy-gauge polyethylene bags before insertion into double-wall corrugated cartons. This protocol protects the thin solid tops from thermal shock, moisture absorption, and fret sprouting during 30 to 45-day ocean container transit.
Accelerate Your Acoustic-Electric Guitar Sourcing Pipeline
Connect directly with our senior luthiery engineering directors and global procurement managers. Whether you require private-label dreadnought production, customized smart preamp electronics, or bulk institutional supply, we deliver verified specifications, stable supply lines, and competitive wholesale pricing.