High-Performance Carbon Fiber & Composite Enclosures
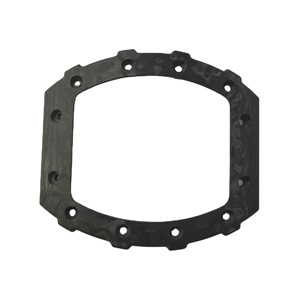
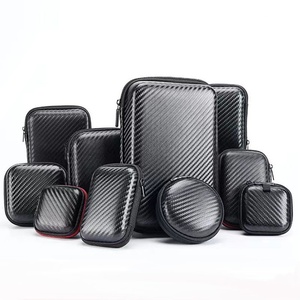
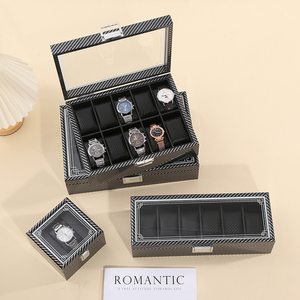
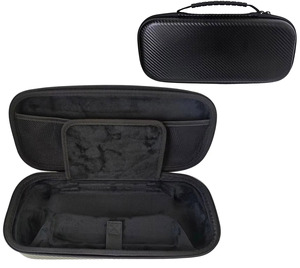
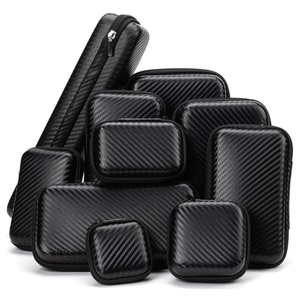
Explore our export-certified product lines ranging from forged carbon luxury watch casings and military-spec EVA tool carriers to ultra-slim ballistic aramid device shells.
Engineering Authority: China's Next-Generation Carbon Composite Manufacturing
As international supply chains place greater emphasis on structural lightweighting, thermal stability, and mechanical strength-to-weight ratios, carbon fiber reinforced polymer (CFRP) enclosures have shifted from boutique luxury novelties into mission-critical protective hardware. As a benchmark China carbon fiber cases manufacturer and global exporter, our facility operates at the intersection of material science, automated composite layup, and high-precision multi-axis subtractive fabrication.
Modern composite engineering demands rigorous resin chemistry formulation, void-free autoclave consolidation, and microscopic defect suppression. While traditional plastic injection molding provides rapid throughput at the cost of high wall-thickness and structural fatigue, continuous-strand carbon fiber fabric impregnated with high-grade epoxy resin provides a tensile strength exceeding 3,500 MPa—nearly five times that of structural steel—at a fraction of the weight. We engineer enclosures for luxury horology, military-grade outdoor instrumentation, commercial consumer electronics, and high-value transport carrying gear.
Advanced Tooling, Prepreg Layup & Autoclave Curing Ecosystem
Our integrated manufacturing plants utilize aerospace-grade dry prepreg carbon fabrics sourced from premier producers like Toray and Mitsubishi. By storing prepregs in -18°C temperature-regulated cleanroom storage units, we preserve resin polymer chain integrity prior to molding. For true structural enclosures, plies are patterned using high-precision CNC laser cut tables and deposited in multidirectional quasi-isotropic laminations (0°/90°/±45°) to counteract torsion, shear stress, and localized puncture risks.
Consolidation is achieved via industrial autoclaves operating at up to 7 bar pressure and continuous thermal cycles at 130°C to 180°C. This extreme positive pressure environment evacuates micro-bubbles and achieves a resin-to-fiber volume ratio of 40:60. The result is an ultra-dense, void-free composite shell ready for 5-axis CNC contour milling, hydrophobic UV-stabilized clear coats, or non-conductive hybrid aramid bonding.
Technical Benchmark: Carbon Fiber Processing Methods Comparison
B2B procurement teams must match performance requirements with manufacturing techniques to optimize costs, unit weights, and tooling investments. The table below outlines our primary production methodologies:
| Manufacturing Technology | Primary Material Matrix | Tensile Strength | Dimensional Tolerance | Ideal B2B Procurement Use Case |
|---|---|---|---|---|
| Autoclave Prepreg Curing | Toray T700/T800 3K/12K Epoxy Prepreg | 3,500 - 4,900 MPa | ±0.05 mm | Aerospace enclosures, high-end drone housings, luxury watch chassis |
| Forged Compression Molding | Chopped Carbon Tow + Vinyl Ester / Epoxy | 1,800 - 2,400 MPa | ±0.02 mm | Complex 3D geometries, ergonomic watch cases, precision structural brackets |
| Thermoformed EVA Composite | High-Density EVA + 3K Textured Carbon PU | 120 - 250 MPa | ±0.50 mm | Field instrument carriers, handheld console luggage, heavy tool bags |
| Vacuum-Assisted Aramid Form | 600D / 1500D Kevlar/Aramid Continuous Filament | 2,800 - 3,200 MPa | ±0.03 mm | Ultra-thin smartphone cases (RF transparent), smart wearable covers |
| Co-Molded Hybrid TPU/CF | Polycarbonate Frame + TPU Bumper + CF Sheet | 350 - 650 MPa | ±0.10 mm | Consumer electronic drop protection, mass-volume corporate tech deployment |
*Data verified via internal tensile testing under ASTM D3039 standards and optical CMM measurement.
Why Global B2B Brands Partner With Our Production Facilities
Decades of manufacturing discipline, vertically integrated production lines, and strict Western quality compliance make us the trusted exporter for tier-1 brands across North America, Europe, and the Asia-Pacific.
End-to-End Vertical Integration
From initial rapid 3D mold tooling, cleanroom prepreg layup, automated CNC finishing, to final Class-100,000 dust-free robotic spray booths, every phase remains entirely in-house.
Zero-Defect Quality Assurance
Every batch undergoes ultrasonic non-destructive testing (NDT) to eliminate internal voids, alongside spectrophotometer color calibration and MIL-STD-810H shock impact validation.
Aramid & Carbon Hybrid Mastery
Expertise in formulating 600D ultra-fine aramid matrices allows zero interference with 5G mmWave signals, Bluetooth, and Qi wireless induction charging modules.
Rapid Prototyping & Agile Tooling
Dedicated CNC tooling centers deliver aluminum production-grade test molds within 10 to 14 business days, reducing new product development cycles by over 40%.
Future B2B Procurement Trends in Carbon Composite Enclosures (2025–2030)
As enterprise procurement managers and supply chain directors prepare for the next decade of hardware innovation, composite sourcing strategies are fundamentally evolving. B2B buyers must navigate changing sustainability mandates, miniaturization demands, and integrated digital supply frameworks.
Circular Composites & Bio-Epoxy Resins
Global regulatory bodies, notably in the European Union, are implementing stringent eco-design and recyclability mandates. Sourcing now leans heavily toward thermoplastic composites (such as CFRTP using PEEK or PPS matrices) that can be repeatedly remelted and reclaimed, as well as bio-resins synthesized from renewable plant oils to drastically reduce cradle-to-gate carbon footprints.
Electromagnetic Transparency & Hybrid Blends
With the proliferation of 5G Advanced, 6G prototypes, and high-frequency IoT sensors, traditional electrical conductivity in carbon enclosures presents severe Faraday-cage shielding challenges. Forward-looking procurement focuses on hybrid cross-weaves pairing true carbon structural cores with precision aramid (Kevlar) windows that permit lossless RF signal transmission.
Agile Digital Twin Tooling & Mold Amortization
Buyers are shifting away from inflexible monolithic tooling commitments. Through cloud-synchronized digital twin simulations and parametric mold designs, Chinese manufacturers now offer modular insert tooling that supports rapid variations in cavity sizing, port layouts, and branding insets without necessitating high capital expenditure for new steel toolsets.
Engineering Trajectories: The Evolution of Carbon Fiber Case Architecture
The manufacturing architecture of protective cases has progressed far beyond rudimentary wet-layup sheets pasted over fiberglass cores. Today's industrial landscape represents a convergence of high-modulus material engineering, computational structural modeling, and surface chemistry:
Forged Composite Aesthetics
Rather than continuous orthogonal weaves, chopped prepreg fibers subjected to extreme hydraulic compression create non-directional, organic damascus patterns with equal multidirectional stiffness.
Nano-Graphene Doped Resins
Infusing graphene nanoplatelets into structural epoxy matrices enhances interlaminar shear strength by up to 28% while accelerating thermal dissipation away from housed internal computing chips.
Sub-Millimeter Thin Walls
Advanced vacuum-compression stamping enables continuous composite wall thicknesses of under 0.60mm while preserving structural drop ratings that surpass 2mm injection-molded ABS/PC plastics.
Ceramic & UV Barrier Coatings
To eliminate surface yellowing and micro-scratching under outdoor solar exposure, proprietary ceramic nanocoatings with 9H pencil hardness ratings are baked directly onto the composite surfaces.
Key Factors When Auditing a Chinese Carbon Fiber Manufacturer
Identifying an experienced composite manufacturing partner in China requires looking beyond sales catalogs. International buyers must evaluate explicit engineering metrics:
- Prepreg Traceability & Resin Uniformity: Confirm that the manufacturer sources certified raw yarns (Toray, Hyosung, or equivalent) and maintains refrigeration batch logs with clear out-time tracking.
- In-House Tooling & 5-Axis CNC Milling: Subcontracting CNC trimming leads to dimensional drift, edge fraying, and extended lead times. Direct control over multi-axis CNC machines ensures pristine cutouts for buttons, hinges, and sealing gaskets.
- Cleanroom Standards for Surface Finishing: Any dust particle embedded beneath clear coats permanently ruins cosmetic grade-A surfaces. Look for cleanroom spray lines and automated optical inspection systems.
- Structural Co-Molding Integrity: If sourcing hybrid cases (e.g., carbon panels bonded to TPU or EVA), inspect the mechanical anchoring groove design and chemical bonding primers to prevent long-term delamination.
Frequently Asked Questions for B2B Importers
Technical clarity regarding production cycles, custom mold investments, RF transparency, and international logistics.
What is the typical Minimum Order Quantity (MOQ) and sample lead time for custom tooling?
How does pure carbon fiber compare to aramid (Kevlar) in smart device enclosures?
What surface finishes and aesthetic weave patterns are available for OEM customization?
What testing certifications and compliance standards do your exported cases satisfy?
Can you co-mold carbon composites with internal EVA foam or magnetic hardware?
How do you manage international shipping, customs, and DDP delivery terms?
Initiate Your Custom Composite Engineering Project
Collaborate with our engineering team to develop lightweight, high-rigidity carbon fiber enclosures tailored to your exact dimensional tolerances, target unit costs, and brand aesthetics.